

 english
 français
 Deutsch
 Italiano
 Русский
 Español
 português
 Nederlandse
 ελληνικά
 日本語
 한국
 العربية
 हिन्दी
 Türkçe
 indonesia
 tiếng Việt
 ไทย
 বাংলা
 فارسی
 polski
PLC parameter input
The listed intelligent touch-screen controller allows welding parameters to be entered and read. Product-position coordinates and process settings are used to define the programmed welding track.

Place of Origin:
China
Brand Name:
Hwashi
Certification:
CE,CCC,ISO
Model Number:
WL-FS -100K

 Video
Video
Video
Hwashi · Resistance Welding Equipment
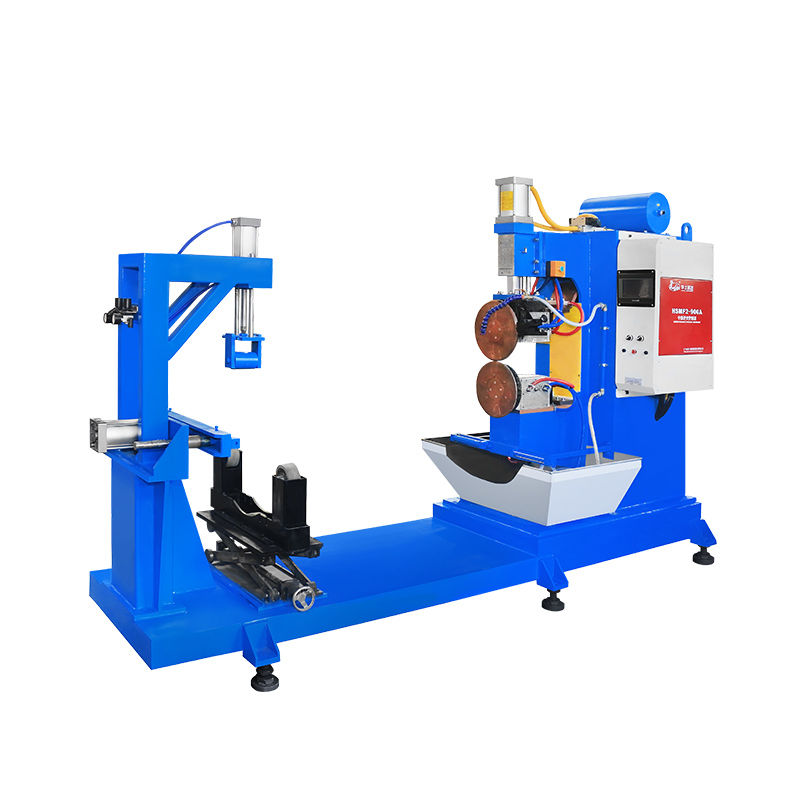
WL-FS-100K pump-motor type configuration for programmed resistance seam welding applications in stainless steel sink production. The machine combines PLC-based parameter input with roller-electrode seam formation.
01 / Product Overview
The Hwashi WL-FS-100K is presented for stainless steel kitchen sink seam welding. Its resistance seam welding process uses a rotating wheel electrode in place of the conventional cylindrical spot-welding electrode. As the wheel travels along the joint, a sequence of overlapping weld nuggets forms a continuous or intermittent seam according to the selected process settings.
The product description identifies a PLC control system for entering welding parameters and product-position coordinates. Once the workpiece is positioned and the preset program is started, the programmed welding track is carried out by the machine. The operator handles workpiece loading and unloading according to the configured production process.
The page title identifies this listing as a pump-motor type sink bowl maker. The actual pump, motor and auxiliary-system configuration should be confirmed against the final machine layout and approved technical proposal.
02 / Technical Specifications
| Parameter | Published value / description |
|---|---|
| Product name | Stainless Steel Kitchen Sink Seam Welding Machine |
| Model | WL-FS-100K |
| Welding process | Resistance seam welding with roller-wheel electrode |
| Control system | PLC |
| Welding width | 5–20 mm |
| Minimum welding thickness | 0.2 mm (as stated in the product listing; application validation is required) |
| Input voltage | 380 V; the listing also states “2 Phase, 50/60 Hz”. Confirm the correct electrical supply and phase arrangement before order. |
| Machine dimensions | 780 × 1250 × 1800 mm |
| Machine weight | 400 kg |
| Machine type | Resistance welding machine |
| Published service-life statement | 8–10 years; actual service life depends on duty cycle, maintenance, operating conditions and consumable replacement. |
| Published minimum order quantity | 1 set |
| Published packaging | Seaworthy wooden packaging |
| Published delivery period | 7–30 working days after receipt of payment; confirm the schedule for the final configuration. |
| Payment terms | T/T, L/C |
| Published supply capability | 50 sets per month (company-stated capacity) |
Specification source: Hwashi WL-FS-100K product listing.
The product page also publishes the following model-family values. These are reference entries for the listed series and should not be interpreted as the confirmed configuration of every WL-FS-100K machine.
| Model | Wheel travel | Input voltage | Input power | Output current |
|---|---|---|---|---|
| WL-FS-15K | Horizontal | 220/380 V | 15 kW | 10,000 A |
| WL-FS-35K | Circular | 220/380 V | 35 kW | 12,000 A |
| WL-FS-50K | Longitudinal | 220/380 V | 50 kW | 12,000 A |
| WL-FS-75K | Horizontal | 380 V | 75 kW | 16,000 A |
| WL-FS-100K | Horizontal | 380 V | 100 kW | 24,000 A |
| WL-FS-MF40K | Circular | 380 V | 40 kW | 19,500 A |
| WL-FS-MF150K | Horizontal | 380 V | 150 kW | 40,000 A |
| WL-FS-MF250K | Longitudinal | 380 V | 250 kW | 50,000 A |
03 / Process & Engineering Features
In resistance seam welding, pressure and electrical current are applied through rotating wheel electrodes. A series of weld nuggets is formed along the joint; the degree of overlap and the selected current pattern determine whether the process is configured for roll spot welding or a more continuous, leak-resistant seam. The source description identifies the principal stages as pressurization, heating/fusion and cooling/solidification.
The listed intelligent touch-screen controller allows welding parameters to be entered and read. Product-position coordinates and process settings are used to define the programmed welding track.
The machine description identifies a copper-alloy wheel electrode. The rotating wheel replaces the conventional spot-welding electrode and supports overlapping weld formation along the joint.
Electrode geometry, extended arms and product fixtures can be designed around the workpiece shape. Special electrode moulds and welding methods are described as configurable to product specifications.
The general seam-welding description states that the welding wheel can operate in horizontal and vertical directions. The actual travel arrangement depends on the selected machine configuration.
The source describes forced-water circulation cooling for the transformer and welding wheel to support operation under the configured load conditions.
The described operating sequence is to locate the workpiece in the designated position, run the preset program and remove the component after the welding cycle is complete.
04 / Product Detail Images
The following images are reproduced from the product-detail image assets associated with the source listing. They provide visual references for the controller, wheel-electrode assembly, seam-welding arrangement and application examples.
Image source: Hwashi product detail page.
05 / Video Demonstration Reference
A demonstration-video reference is provided as supplementary visual context for buyers reviewing the equipment and its production application. It complements the written description of the resistance seam-welding process, programmed operation and workpiece handling. The video is referenced as an external source only; no embedded player or video container is used in this product description.
Video data source
YouTube video reference — OH6DXNm3gdY
06 / Applications & Configuration
The product is listed for stainless steel kitchen sink seam welding. The wider seam-welding platform description also references sheet metal, barrel bodies, boxes and sealed thin-wall containers. Other application examples named by the manufacturer include fuel tanks, motorcycle dampers, temperature-control components, battery nickel strips, water-pump components and metal containers.
For a sink-specific project, the tooling and process should be evaluated against the actual material grade, sheet thickness, joint geometry, sink dimensions, required seam location and production takt. A representative workpiece sample and drawing are useful inputs for process trials and fixture design.
07 / Manufacturer Profile
Guangdong Hwashi Technology Inc. describes itself as a manufacturer and solution provider focused on automatic resistance-welding equipment and industrial robotics. The company profile states that it was established in 2001 and serves applications across home appliances, kitchen utensils, wire and cable products, lighting, metal hardware, electronics and automotive components.
The factory profile identifies production facilities in Huizhou, Guangdong and Gao'an, Jiangxi, and describes capabilities covering resistance-welding machines, automated welding lines and industrial robots. These are company-level manufacturing statements rather than machine-specific performance certifications.
Company information and updates can also be cross-referenced through the Hwashi Technology Facebook page. A social-media page is an additional brand-presence reference and is not a substitute for corporate registration, factory audit or product compliance documents.
Company and certification sources: Company profile · Factory profile · Quality and certificate information.
08 / Trade Data & Fulfillment Context
Public trade-data sources contain supplier-name records associated with Guangdong Hwashi Technology Inc. The records below are summarized at company level and are not evidence that the WL-FS-100K sink-welding machine was shipped in those transactions.
Trade-data sources: ImportGenius supplier profile · ECER supplier trade-data reference.
| Period | Consolidated product category & HS code | Target region / market | Consolidated shipment profile |
|---|---|---|---|
| July 2025 | Automatic welding and cutting machinery for copper-wire applications; HS 85152190 | India | One industrial-equipment shipment described in the ECER record as a 100 kVA AC-powered automatic welding and cutting machine. |
| Nov 2006 – Nov 2026 database coverage | Supplier profile reports 15 shipment entries; detailed product-category consolidation is not available in the public summary. | United States import-data profile; Long Beach shown as the top port | 15 total shipments and 10 trading partners shown under the supplier-name variant “Guangdonghwashi Technology Inc.” |
The shipment information shown is a selective set of representative records available from public trade and shipment databases and does not constitute the supplier's complete shipping history. Records are associated through supplier-name matching and related name forms, then summarized into high-level category references for ECER-indexed context. Corporate spelling variations, subsidiaries, related entities and duplicate registrations may occur. These records are provided for reference only and do not formally verify or endorse supplier creditworthiness, qualifications, product quality or the identity of every shipment. Buyers should independently cross-check any transaction relied upon during formal due diligence against primary commercial documents, including bills of lading, customs declarations and commercial invoices.
09 / Buyer FAQ
The product description states that machine structure, extended arms, electrode moulds and welding methods can be designed according to the workpiece. Buyers should provide sink drawings, dimensions, material grade, thickness range and seam-location details so the proposed tooling and working envelope can be reviewed.
Provide the stainless-steel grade, thickness, surface condition, joint design and sample parts. Welding current, wheel pressure, speed, pulse pattern and cooling conditions should be established through engineering trials. The published minimum thickness of 0.2 mm should be treated as a listing value and validated for the buyer's actual material and joint.
Define the critical dimensions, allowable distortion, seam appearance, joint strength and any leak-tightness requirement in the technical agreement. A sample-welding evaluation and mutually approved inspection plan should be completed before mass production. No universal tolerance or weld-strength value is assumed in this page.
The product listing specifies seaworthy wooden packaging. Before shipment, buyers should confirm the packing design, moisture barrier, desiccant, corrosion protection for exposed metal surfaces, immobilization of moving parts, shock protection and the packing-list details for accessories and spare parts.
Agree the required document list before order placement. Depending on the supplied materials and project scope, buyers may request a factory inspection record, electrical test record, machine run-off report, sample-welding report or third-party inspection. Material Test Certificates (MTCs) should be requested where material traceability is part of the purchase specification; availability should be confirmed for each item.
The product page publishes a delivery period of 7–30 working days after payment. Actual timing depends on the approved configuration, tooling, component availability and inspection schedule. The purchase contract should state the agreed lead time, shipment readiness date, acceptance milestones and the consequences of schedule changes.
Hwashi's company profile describes online troubleshooting, operating guidance and technical support, and states a standard one-year warranty after shipment. Buyers should obtain the warranty terms in writing, including covered components, exclusions, response procedure, remote-support arrangements, spare-parts supply and any on-site service costs.
10 / Before Order Confirmation
Video
Video
Send your inquiry directly to us